


Industrial PLC – What Is It, How Does It Work and What Is Its Role in Industrial Automation?
Industrial PLCs – What Are They, How Do They Work and What Is Their Role in Industrial Automation?
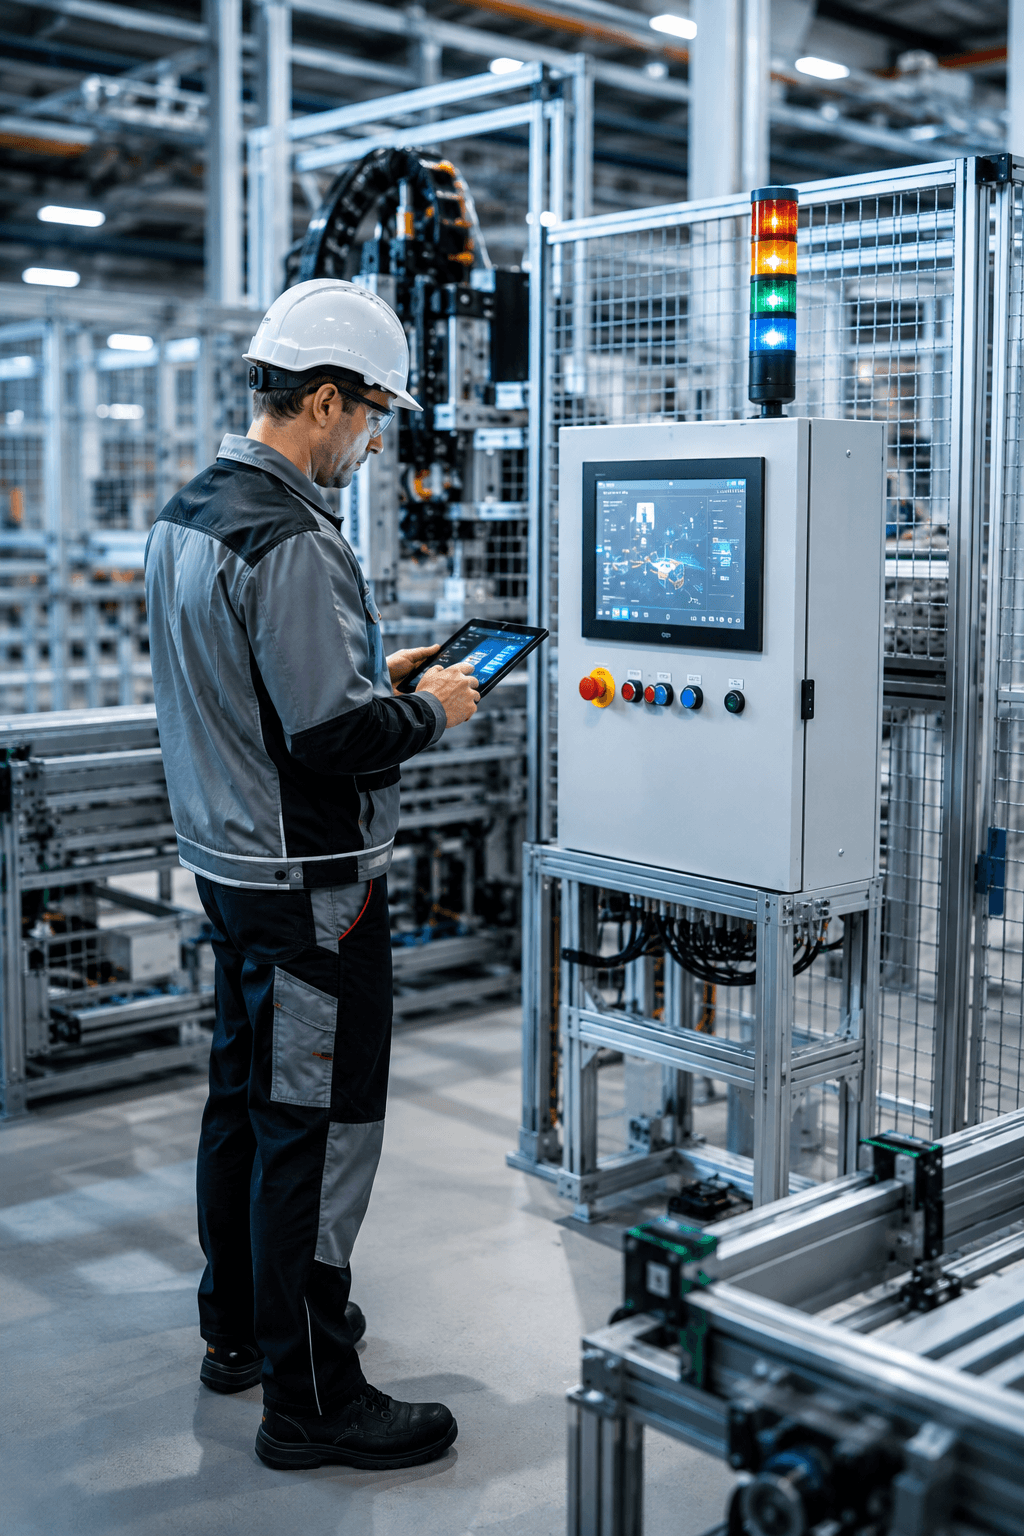
Industrial process automation enables precise equipment control, monitoring of operating parameters and reduced manual intervention. At the heart of many automation systems is the industrial PLC, a programmable electronic device used to control machinery and industrial processes.
An industrial PLC, also known as a programmable logic controller, receives information from sensors and other input devices, processes it according to a program and sends commands to motors, valves, actuators or other system components. Thanks to their robust construction and programming flexibility, these controllers are used across numerous industries.
This article explains how a PLC works, its main components, programming languages, industrial applications and the criteria to consider when selecting the right controller for an automation system.
Programmable logic controllers automate operating sequences, monitor equipment and adapt processes to production requirements. Integrating them with sensors, electric drives and operator interfaces helps industrial systems operate in a coordinated way.
Contents
- What Is an Industrial PLC and How Does It Work?
- What Are the Main Components of an Industrial PLC?
- How Is an Industrial PLC Programmed?
- Where Are PLCs Used in Industrial Automation?
- How Do You Choose the Right Industrial PLC for Your Application?
- Industrial PLCs and the Integration of Automation Components
1. What Is an Industrial PLC and How Does It Work?
An industrial PLC (programmable logic controller) is an electronic device designed to automate and control industrial processes. It receives signals from sensors, pushbuttons and other devices, processes the information according to a program and sends commands to system components.
Unlike traditional control systems based on electromechanical relays, a PLC allows the operating logic to be modified through programming without completely rewiring the electrical circuits. This flexibility makes it easier to adapt systems to new production requirements and integrate additional monitoring and control functions.
PLCs are designed for industrial environments and can operate under conditions involving vibration, electromagnetic interference and temperature variations, within the limits specified by the manufacturer. They are found in automated production lines, processing machinery, conveyor systems and many other industrial applications.
1.1. How an Industrial PLC Works
A programmable logic controller works by processing information received from connected equipment. In a typical application, the PLC reads the input states, executes the control program and updates the outputs that control equipment in the system.
The process can be divided into three main stages:
- Reading the inputs: the PLC receives information from proximity sensors, temperature sensors, pressure transducers, pushbuttons or other devices. Signals may be digital, indicating discrete states, or analog, representing measured values.
- Executing the program: the processor analyzes the received data and executes the instructions defined in the automation program. During this stage, it evaluates logical conditions, timing functions, measured values and operating sequences.
- Updating the outputs: based on the program results, the PLC sends commands to contactors, solenoid valves, variable frequency drives or other actuation devices.
In many controllers, these operations are repeated in a scan cycle. The cycle time depends on the PLC model, program complexity and system configuration. Some applications also use interrupts, periodic tasks or dedicated modules for operations with specific response time requirements.
On a production line, a sensor detects a product on the conveyor belt and sends a signal to the PLC. The controller checks the programmed instructions and can command the drive system to start, stop or change the belt speed. At the same time, it can monitor other operating conditions and send information to the operator interface.
1.2. What Types of Signals Can a PLC Process?
An industrial PLC can use several types of inputs and outputs, depending on the installed modules and application requirements. Selecting the right types is important for compatibility with the sensors, actuators and other equipment in the automation system.
- Digital inputs: indicate discrete states, such as on/off or presence/absence. They are used for pushbuttons, contacts and sensors with digital outputs.
- Digital outputs: send commands to relays, contactors, indicator lights or other compatible devices.
- Analog inputs: allow variable values, such as temperature, pressure or tank level, to be read through standardized signals, for example 0–10 V or 4–20 mA.
- Analog outputs: transmit control values to compatible equipment, such as certain variable frequency drives or regulators.
- Communication interfaces: enable data exchange with HMI interfaces, SCADA systems, electric drives and other controllers through compatible protocols.
Not all PLCs provide all these functions in their standard configuration. Some models include integrated inputs and outputs, while others require additional modules to expand their control and communication capabilities.
1.3. What Is the Difference Between a PLC and an Industrial Computer?
Both PLCs and industrial computers can be used in process automation, but their architecture and implementation differ. A PLC is primarily designed to control equipment through industrial inputs and outputs, while an industrial computer can be used for complex software applications, processing large volumes of data or process visualization.
PLCs generally provide a runtime environment dedicated to automation, with diagnostic capabilities and integration of input and output modules. Industrial computers can offer greater software flexibility, but the implementation of real-time control functions depends on the operating system, software platform and architecture used.
The two technologies are not mutually exclusive. In many installations, the PLC controls the equipment, while the industrial computer is used for monitoring, data collection or integration with other information systems.
1.4. Main Benefits of Using an Industrial PLC
Integrating a PLC into an automation system can offer several operational benefits, depending on the installation configuration and the design of the control program.
- Programming flexibility: operating sequences can be adapted when industrial process requirements change.
- Equipment integration: the controller can coordinate sensors, motors, actuators and other components through its available interfaces.
- Monitoring and diagnostics: diagnostic functions help identify certain faults and monitor operating states.
- System expansion: modular controllers can support additional inputs, outputs and communication interfaces.
- Process repeatability: automatic execution of programmed sequences helps maintain consistent operating conditions.
A standard PLC does not automatically replace dedicated functional safety systems. For functions such as emergency stopping or monitoring access to hazardous areas, the safety architecture must be determined based on risk assessment and applicable requirements. Depending on the application, safety controllers and certified components may be required.
To understand how these functions are implemented, it is important to examine the controller architecture and the role of each component. The next chapter covers the processor, memory, power supply, input and output modules, and communication interfaces of an industrial PLC.
2. What Are the Main Components of an Industrial PLC?
An industrial PLC consists of several hardware and software components that work together to monitor and control automated processes. The exact configuration varies depending on the manufacturer, model and application complexity, but the basic principles are similar for most programmable logic controllers.
Depending on its design, a PLC may be compact, with the processor, power supply, inputs and outputs integrated into a single unit, or modular, with separate components that allow system expansion. Understanding the architecture is important both when designing new installations and when troubleshooting or upgrading existing systems.
2.1. Central Processing Unit (CPU)
The central processing unit, known as the CPU, is responsible for executing the automation program. It processes information received from the inputs, performs the necessary logical and mathematical operations and determines the commands to be sent to the outputs.
The main processor functions include:
- Program execution: interpreting and executing the instructions that define how the system operates.
- Data processing: performing logical, arithmetic, timing and counting operations.
- Input and output management: receiving information from connected devices and sending the appropriate commands.
- System diagnostics: detecting certain hardware, communication or program execution faults.
- Communication management: exchanging information with other controllers, HMI interfaces and compatible industrial equipment.
Processor performance affects program execution time and the controller's ability to handle complex applications. When selecting a PLC, consider execution time, memory capacity, the number of supported modules and the available technology functions.
2.2. PLC Memory and Program Storage
An industrial PLC's memory stores the control program, configuration parameters and data required for system operation. Memory architecture varies between manufacturers, but modern controllers generally use separate areas for the program and process data.
Some variables are continuously updated during operation, while others can be configured to retain their values after a power interruption. This function is useful for production counters, process parameters or certain states that must be restored when the equipment restarts.
Memory capacity should be selected according to program size, the number of variables, diagnostic functions and any planned system expansions.
2.3. Input and Output (I/O) Modules
Input and output modules connect the PLC to equipment in the industrial installation. They receive signals from sensors and send commands to actuation devices.
Depending on the application, the following may be used:
- Digital input modules: for reading pushbuttons, proximity sensors, contacts and other discrete signals.
- Digital output modules: for controlling contactors, relays, indicators and other compatible equipment.
- Analog input modules: for measuring temperature, pressure, level or other parameters represented by analog signals.
- Analog output modules: for transmitting control values to regulators, drives and other devices.
- Technology modules: for applications requiring high-speed counting, position measurement, motion control or other specialized functions.
In modular systems, I/O modules can be located beside the CPU or distributed near the controlled equipment and connected through industrial networks. Using distributed I/O can reduce cable lengths and simplify system expansion.
The number of channels is not the only important criterion. Check the supply voltage, signal types, permissible current, analog input resolution, electrical isolation and module compatibility with the PLC model used. It is also advisable to reserve spare channels for potential system expansions.
2.4. Power Supply
The power supply provides the electrical power needed to operate the controller and, depending on the configuration, certain associated modules. Many industrial PLCs use a 24 V DC supply, although models designed for other voltages are also available.
When sizing the power supply, account for the consumption of the CPU, expansion modules and devices powered by the same supply. Circuit protection, grounding and compliance with the manufacturer's recommendations for installation in the electrical control cabinet are also important.
2.5. Communication Interfaces and Modules
Modern automation systems require data exchange between controllers, smart sensors, electric drives, operator interfaces and monitoring platforms. For this purpose, PLCs may have integrated communication ports or use additional modules.
Protocols and technologies used in industrial automation include:
- PROFINET: used for industrial Ethernet communication between controllers and compatible equipment.
- Modbus TCP and Modbus RTU: protocols used to exchange data between many types of industrial equipment.
- EtherNet/IP: used in automation systems that integrate devices compatible with this technology.
- EtherCAT: used, among other applications, where fast communication and equipment synchronization are required.
- OPC UA: used for structured data exchange between equipment and software systems, depending on the implementation.
Support for these protocols varies by model. Some controllers support them directly, while others require additional modules, licenses or communication devices.
2.6. Compact or Modular PLCs – What Are the Differences?
In terms of design, programmable logic controllers can be divided into two main categories: compact PLCs and modular PLCs.
Compact PLCs integrate the main components into a single unit and are frequently used in applications with a relatively small number of inputs and outputs. They can be suitable for individual machines and installations with clearly defined automation requirements.
Modular PLCs allow the system to be configured by selecting the CPU, I/O modules and communication interfaces. This architecture offers flexibility for complex installations and applications that require future expansion.
A PLC configuration should be determined by the number and type of signals, communication requirements, response time and expansion options. Selecting the right architecture during the design stage can simplify subsequent maintenance and system upgrades.
The hardware components determine the controller's capabilities, but the automation program defines how the system behaves. The next chapter examines the main PLC programming languages, the stages of program development and the importance of testing before commissioning.
3. How Is an Industrial PLC Programmed?
Programming an industrial PLC involves defining the instructions that enable the controller to monitor input signals, process data and control connected equipment. The program determines the sequence of operations, start and stop conditions, timing functions and system responses to different events.
Programs are generally developed in a software environment specific to the manufacturer or automation platform. Before implementation, the process requirements, equipment configuration and system operating conditions must be defined.
3.1. Main PLC Programming Languages
The IEC 61131-3 standard defines languages used to program industrial controllers. The choice of language depends on the PLC platform, application complexity and the experience of the team developing and maintaining the system.
Ladder Diagram (LD)
Ladder Diagram is a graphical language inspired by relay circuit diagrams. Instructions are represented by contacts, coils and other graphical elements that describe the logical conditions of the process.
It is frequently used for start and stop commands, interlocks, timing functions and logical sequences. Its graphical representation can make the program easier to understand for personnel familiar with industrial electrical schematics.
Function Block Diagram (FBD)
Function Block Diagram is a graphical language in which functions are represented by interconnected blocks. Each block receives specific input data, performs an operation and passes results to other program elements.
This language is used to implement logical functions, calculations and certain control algorithms. A block-based structure allows functions to be reused and automation applications to be organized clearly.
Structured Text (ST)
Structured Text is a high-level textual language with instructions for logical operations, calculations, conditions and loops. It is suitable for algorithms involving numerous variables, mathematical formulas or the processing of data structures.
In complex applications, Structured Text can be used alongside graphical languages, depending on the capabilities of the programming environment.
Sequential Function Chart (SFC)
Sequential Function Chart allows a process to be organized into steps and transitions. It is useful for installations where operations must be performed in a specific order, such as assembly lines, dosing systems or automatic machine cycles.
The transition from one step to another occurs when the conditions defined in the program are met. Availability and implementation depend on the platform used.
No single language suits every application. Ladder Diagram can be useful for control logic, Function Block Diagram for interconnecting functions, Structured Text for complex algorithms and Sequential Function Chart for sequential processes. In industrial projects, these methods can be combined to create a clear, maintainable program.
3.2. Stages of PLC Program Development
Programming an industrial controller does not begin with writing instructions. Proper implementation requires analysis of the industrial process and a definition of how the equipment should operate.
- Requirements analysis: identifying the operations to automate, the parameters to monitor and the operating conditions.
- Defining inputs and outputs: creating a list of the sensors, pushbuttons, actuators and other devices to be connected to the PLC.
- Control logic design: defining operating sequences, timing functions, interlock conditions and error handling.
- Program development: implementing the logic in a software environment compatible with the selected PLC model.
- Simulation and testing: checking program operation and identifying potential errors before use on the actual installation.
- Commissioning: checking connections, testing equipment and validating system behavior under controlled conditions.
- Documentation and maintenance: retaining program versions, the hardware configuration and information needed for future work on the system.
In complex industrial applications, these stages involve collaboration between PLC programmers, electrical engineers, automation specialists and the personnel responsible for operating the equipment.
3.3. Practical Example of Industrial PLC Programming
To understand the principle of programming, consider a simplified application in which a PLC controls an electric motor that drives a conveyor belt.
The system may include the following components:
- A pushbutton to start the conveyor belt.
- A pushbutton for a normal process stop.
- A sensor to detect products.
- An electric motor and compatible drive equipment.
- An industrial PLC with the required inputs and outputs.
The program can be configured so that pressing the start pushbutton activates the motor command, provided the system is ready to operate. The sensor supplies information about product presence, and the PLC can use this data for counting, timing or coordinating subsequent process stages.
When the normal stop pushbutton is pressed, the program deactivates the motor command according to the defined sequence. Emergency stop functions and other safety measures must be designed separately, based on risk assessment and applicable safety requirements.
3.4. Software Environments Used for PLC Programming
Each manufacturer or automation platform may use its own software environment to configure and program controllers. These applications support program development, module configuration, communication setup and equipment diagnostics.
Well-known examples include:
- Siemens TIA Portal: a platform used to configure and program compatible Siemens controllers.
- Rockwell Automation Studio 5000: an environment used to develop applications for certain Allen-Bradley controller families.
- CODESYS: a development platform used by numerous automation equipment manufacturers.
- Bosch Rexroth ctrlX WORKS: an engineering environment used to configure and develop applications on the ctrlX AUTOMATION platform.
The choice of software environment depends on compatibility with the installed equipment, the functions required and project requirements. Before purchasing a PLC, also check the licensing terms, supported software versions and availability of diagnostic tools.
3.5. Testing, Diagnosing and Updating PLC Programs
Once the program has been developed, testing is essential to verify operating sequences and identify errors. Depending on the platform, simulation tools, variable monitoring and diagnostic functions integrated into the software environment may be available.
Testing must cover both normal operation and system behavior in situations such as signal loss, communication interruption or values outside acceptable limits. Safety functions are validated according to the procedures and requirements specific to the installation.
During operation, program changes must be documented and managed through a version control process. Keeping backups of the program and configuration can reduce the time needed to restore the system after a controller failure or maintenance work.
A well-documented program makes troubleshooting, maintenance and subsequent system modifications easier. Clear variable names, relevant comments, up-to-date electrical schematics and retained backups are important for industrial process continuity.
Programming is just one stage of implementing an automation system. The next chapter examines the main areas where industrial PLCs are used and how they coordinate equipment and industrial processes.
4. Where Are PLCs Used in Industrial Automation?
An industrial PLC can be integrated into a wide range of equipment and installations, from individual machines to complex production lines. By processing sensor signals and coordinating actuation devices, programmable logic controllers automate repetitive operations and monitor industrial processes.
Programming flexibility and connectivity to industrial networks make PLCs suitable for numerous sectors, including automotive manufacturing, metalworking, food processing and material handling.
4.1. Production Lines and Conveyor Systems
In automated factories, PLCs coordinate conveyor belts, sorting systems, assembly stations and other production equipment. They can control the sequence of operations, monitor product presence and synchronize multiple machines.
Integration with sensors and variable frequency drives allows conveyor speed and operating sequences to be adjusted to process requirements.
4.2. Industrial Machinery and Hydraulic Systems
Programmable controllers are also used to automate presses, processing machines and hydraulic installations. In these applications, the PLC can monitor pressure, position and temperature, sending commands to solenoid valves, pumps and other system components.
Proper integration of electrical and hydraulic components enables coordinated movement and control of operating parameters. For more information about this equipment, visit the dedicated hydraulic applications page at CreatX Technology.
4.3. Food Processing and Packaging Systems
In the food industry, PLCs are used to control dosing, filling, packaging and conveying systems. They can coordinate operations based on sensor information and the parameters defined for each process stage.
4.4. Process Monitoring and Control Systems
PLCs can be connected to HMI interfaces and SCADA systems to display parameters, manage alarms and monitor equipment. Depending on the system architecture, the collected data can also be used for performance analysis or maintenance planning.
The efficiency of an automation system depends on compatibility between the controller, sensors, drives and communication equipment. Selecting the right components simplifies integration and allows the system to be adapted to future production requirements.
5. How Do You Choose the Right Industrial PLC for Your Application?
An industrial PLC should be selected according to the installation's technical requirements, process complexity and the equipment to be controlled. A suitable controller must provide the resources needed for the current application and, where relevant, allow future system expansion.
5.1. Number and Type of Inputs and Outputs
The first step is to identify all sensors, pushbuttons and actuation devices that need to be connected. This determines the required number of digital or analog inputs and outputs, as well as any specialized modules.
For installations that may be expanded later, it is useful to select a controller with spare capacity or the option to add I/O modules.
5.2. Processor Performance and Memory Capacity
Execution time, memory capacity and available technology functions must match the complexity of the program. Applications requiring motion control, rapid signal processing or coordination of multiple devices may have higher performance requirements.
5.3. Compatibility with Existing Equipment
When upgrading an installation, check the PLC's compatibility with existing sensors, variable frequency drives, servo motors and monitoring systems. The available communication protocols can affect both integration costs and project complexity.
5.4. Operating Conditions and Maintenance
Compare ambient temperature, humidity, vibration and installation conditions with the manufacturer's specifications. Spare parts availability, access to technical documentation and the ability to back up the program are also important.
Before selecting an industrial PLC, determine the number of inputs and outputs, performance requirements, communication protocols, environmental conditions and expansion options. The total cost should also include additional modules, software licenses and integration into the existing installation.
Controller selection is one part of automation system design. To ensure correct operation, assess how the other industrial components will be integrated, from sensors and drives to communication equipment.
6. Industrial PLCs and the Integration of Automation Components
An industrial PLC is the control unit of an automated system, but the operation of the entire installation depends on correct integration of all components. Sensors, motors, electric drives, hydraulic equipment and communication interfaces must be compatible with the selected automation architecture.
In modern installations, the controller can coordinate several devices simultaneously, monitor process parameters and send information to supervisory systems. Integration must reflect the technical and operational requirements of each application.
6.1. Integrating Sensors and Drive Systems
Sensors provide the information needed for process control, while drive and actuation systems carry out commands sent by the PLC. Depending on the application, these may include servo motors, variable frequency drives, pneumatic cylinders or hydraulic components.
For correct integration, check each device's signal types, communication protocols, response times and power supply requirements.
6.2. The Role of PLCs in Hydraulic System Automation
In industrial hydraulic applications, PLCs can coordinate pumps, solenoid valves and actuators using information from pressure, temperature and position sensors. This integration enables automated operating sequences and monitoring of system parameters.
For more information about the equipment used in these systems, explore the range of Bosch Rexroth hydraulic pumps and the dedicated page on hydraulic applications.
6.3. Industrial Communication and Equipment Monitoring
Through industrial networks, PLCs can communicate with other controllers, HMI interfaces, SCADA systems and smart devices. This information exchange enables centralized process monitoring, parameter logging and identification of certain operating anomalies.
For existing installations, upgrading the automation system may involve integrating additional communication modules or replacing components that no longer meet application requirements.
When designing or upgrading an automation system, verify compatibility between the PLC, sensors, drives and industrial equipment using the technical documentation. Selecting the right components can simplify integration, maintenance and future expansion.
Conclusion: The Role of PLCs in Modern Industrial Automation
An industrial PLC is an important component of modern automation systems, used to control machinery, monitor parameters and coordinate industrial processes. Selecting the right controller depends on application complexity, the number of inputs and outputs, required performance and compatibility with existing equipment.
For efficient system operation, the controller must be properly integrated with sensors, drive systems and other industrial components. Technical documentation, testing and maintenance planning support long-term operation and future system upgrades.
Looking for Components for Your Industrial Equipment?
At CreatX Technology, you can explore the range of available industrial equipment and components. If you need a specific part, send us the manufacturer's part number or the equipment's technical specifications to request information about availability and compatibility.
Discover the solutions available for your industrial applications or contact the CreatX Technology team to request a quotation.
Request a Quote Explore Hydraulic ApplicationsRelated posts
-
 Industrial Automation
Bosch Rexroth industrial automation solutions help increase productivity, optimize manufacturing processes and...Read more
-
 ctrlX AUTOMATION
 is the Bosch Rexroth automation ecosystem that integrates control, motion, I/O and software into a...Read more
-
 How to Identify Whether the Problem Is the PLC, Sensor, Motor or Gearbox?
Discover how to quickly identify whether a fault originates from the PLC, sensor, motor or gearbox, and learn the...Read more
-
 Industrial Automation Maintenance – How to Prevent Failures and Unplanned Downtime?
Discover how an effective industrial automation maintenance strategy can prevent failures, reduce unplanned downtime,...Read more
Leave a comment